How Does Food Grade Silicone Oil Work as a Defoamer?
Foam is a common problem in food processing. It can form during mixing, pumping, heating, fermentation, filling, and other operations where air becomes dispersed in a liquid. Excessive foam can reduce tank capacity, interfere with level control, cause overflow, and slow production.
Food grade silicone oil, typically based on polydimethylsiloxane (PDMS), is used as a defoamer because of its low surface tension, hydrophobicity, chemical stability, and ability to destabilize the thin liquid films surrounding gas bubbles.
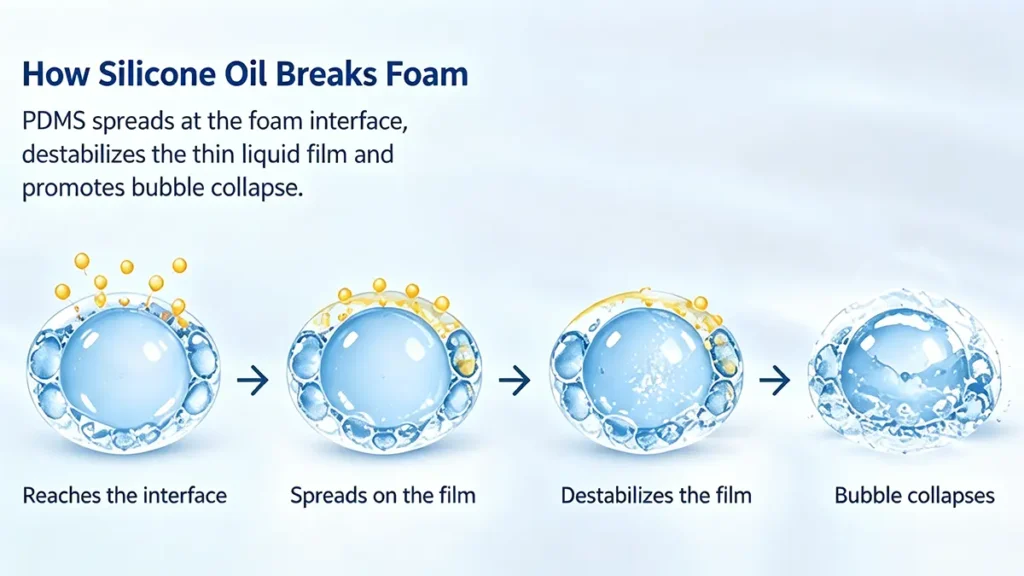
The basic mechanism is physical: the silicone phase reaches the foam interface, spreads or enters the foam film, destabilizes the film, and promotes bubble collapse. In PDMS-silica antifoams, the solid silica phase can further contribute to foam-film rupture through a bridging-related mechanism. Research has shown that PDMS-based antifoam performance is strongly affected by surfactant adsorption and interfacial properties.
Silico® Food Grade Silicone Oil provides high-purity PDMS silicone fluid options for selected food-processing and defoaming applications. The appropriate grade should be selected according to the process liquid, viscosity, dosing method, required foam-control performance, and applicable food regulations.
Table of Contents
- 1. What Causes Foam in Food Processing?
- 2. What Is Food Grade Silicone Oil?
- 3. Why Is PDMS Effective as a Defoamer?
- 4. How Does Silicone Oil Break Foam?
- 5. The Main Stages of Silicone Defoaming
- 6. Why Does Surface Tension Matter?
- 7. Does Silicone Oil Viscosity Affect Defoaming?
- 8. Silicone Oil vs. Silicone Antifoam
- 9. Food Processing Applications
- 10. How Much Silicone Defoamer Should Be Used?
- 11. Food Contact and Regulatory Requirements
- 12. How to Select Food Grade Silicone Oil for Defoaming
- 13. Common Problems with Silicone Defoamers
- Conclusion
1. What Causes Foam in Food Processing?
Foam forms when gas becomes dispersed in a liquid and the resulting bubbles are stabilized by surface-active substances.
Common causes in food processing include:- High-speed mixing
- Pumping and circulation
- Fermentation
- Agitation
- Heating
- Filling and transfer
- Proteins
- Surfactants and emulsifiers
- Sugars and syrups
A foam bubble consists of a gas phase surrounded by a thin liquid film. Proteins, surfactants, and other surface-active materials can accumulate at this interface and make the film more resistant to drainage and rupture.
Excessive foam can lead to:- Reduced tank capacity
- Product overflow
- Unstable level measurements
- Reduced processing efficiency
- Product loss
- Difficult filling and packaging
- Longer cleaning cycles
A defoamer therefore does more than simply remove air. Its main function is to destabilize the foam structure so existing bubbles collapse and new foam formation is reduced.
2. What Is Food Grade Silicone Oil?
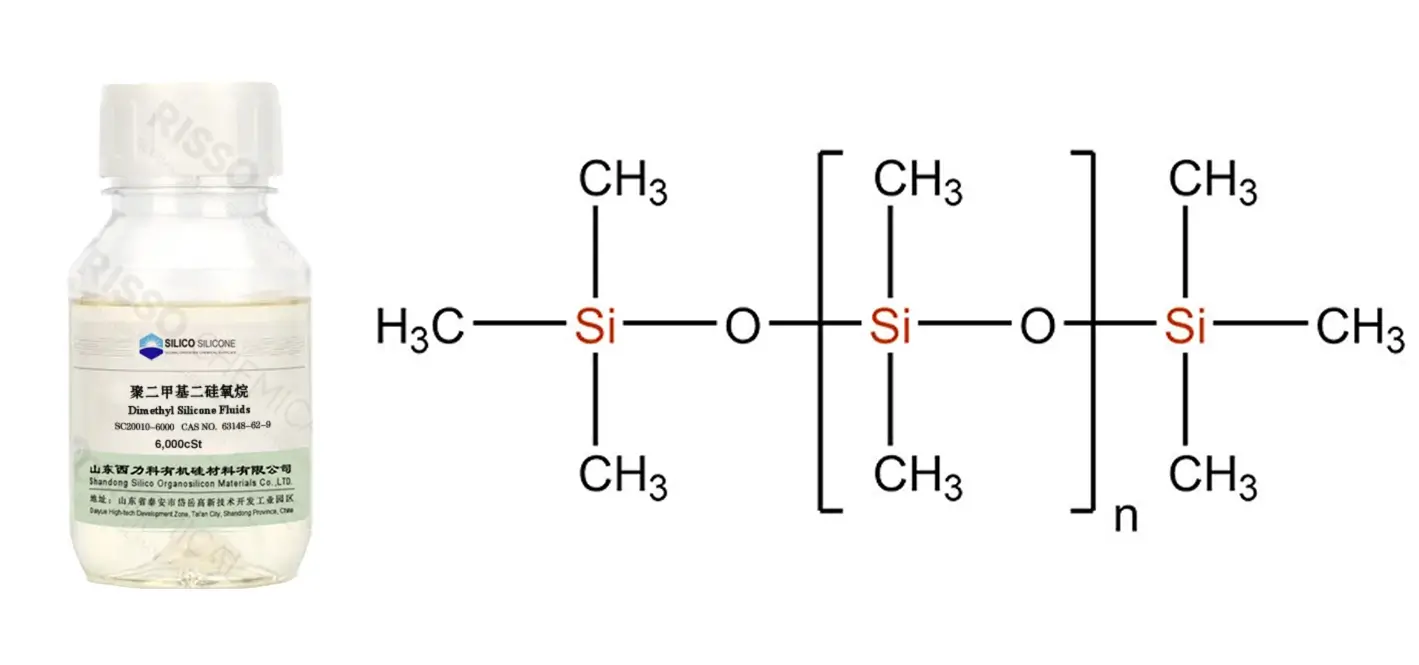
Food grade silicone oil used for foam control is generally based on polydimethylsiloxane (PDMS), also known as dimethylpolysiloxane or dimethyl silicone fluid.
The basic PDMS structure is:
–[Si(CH₃)₂–O]ₙ–
Its silicon-oxygen backbone and methyl groups provide several properties useful for foam control:| Property | Relevance to Defoaming |
|---|---|
| Low surface tension | Promotes interfacial spreading |
| Hydrophobicity | Helps maintain a separate silicone phase |
| Chemical stability | Supports use under different process conditions |
| Controlled viscosity | Affects flow and dispersion |
| Low water solubility | Helps maintain an antifoam phase |
| Interfacial activity | Allows interaction with foam films |
The Codex GSFA identifies polydimethylsiloxane as INS 900a and lists antifoaming agent as one of its functional classes. Its permitted levels vary by food category and use
3. Why Is PDMS Effective as a Defoamer?
PDMS is effective because of its interfacial properties.
Its surface tension is approximately 21 mN/m at ambient temperature, considerably lower than that of water. This allows PDMS to spread effectively at suitable interfaces.
For a silicone-based defoamer to work efficiently, it generally needs to:
- Reach the foam interface.
- Enter or spread across the foam film.
- Disturb the structure of the film.
- Promote film thinning and rupture.
- Reduce the persistence of existing and newly formed foam.
The effectiveness depends on the complete system, not just the silicone oil itself. Surfactants, proteins, oils, salts, temperature, and other components of the process liquid can change the behavior of the foam and the defoamer. Research on PDMS-silica antifoams has shown that surfactant adsorption layers can strongly influence antifoam activity.
4. How Does Silicone Oil Break Foam?
4.1. The Silicone Phase Reaches the Foam
Silicone oil must move from the bulk liquid to the air-liquid interface.
Because PDMS has limited water solubility, it can remain as a separate phase rather than dissolving completely into the aqueous system.
4.2. The Silicone Spreads at the Interface
Once it reaches a suitable interface, the low surface tension of PDMS promotes spreading.
This changes the local interfacial conditions and can accelerate foam-film destabilization.
4.3. The Foam Film Becomes Unstable
The silicone phase interferes with the thin liquid film surrounding the bubble.
For PDMS-based antifoams containing hydrophobic silica, studies describe the action as bridging-stretching, where unstable oil bridges contribute to foam-film rupture.
4.4. The Bubble Collapses
Once the foam film loses sufficient stability, it ruptures and the gas escapes.
The overall process can therefore be summarized as:
PDMS reaches interface → spreads/enters film → destabilizes film → film ruptures → bubble collapses
5. The Main Stages of Silicone Defoaming
5.1 Entry
The antifoam must reach the foam film.
If droplets remain poorly dispersed in the bulk liquid, foam-control efficiency may be reduced.
5.2 Spreading
The silicone phase must spread effectively across the interface.
Strong surfactant adsorption can hinder this process. Studies of PDMS-based antifoams show that the structure and density of surfactant adsorption layers influence both antifoam activity and durability.
5.3 Film Rupture
Once the silicone phase interacts effectively with the foam film, interfacial forces can cause film thinning and rupture.
In PDMS-silica systems, the silica particles can help lower the barrier for antifoam entry and contribute to foam-film destabilization.
6. Why Does Surface Tension Matter?
Surface tension is an important factor in silicone defoaming.
PDMS has a surface tension of approximately 21 mN/m, while water is around 72 mN/m at room temperature.
This difference helps explain why PDMS can spread readily at appropriate interfaces.
However, low surface tension alone does not guarantee effective defoaming.
Performance also depends on:
- Spreading behavior
- Entry into the foam film
- Droplet size
- Viscosity
- Hydrophobicity
- Surfactant concentration
- Process temperature
- Antifoam formulation
For example, a highly stabilized protein or surfactant foam may respond differently from a simple aqueous solution.
7. Does Silicone Oil Viscosity Affect Defoaming?
- Easier pumping
- Easier metering
- Faster spreading
- Easier dispersion
- Greater film retention
- Slower flow
- Different dispersion behavior
- More persistent surface films
Higher viscosity does not automatically mean better defoaming.
The correct viscosity depends on the process, dosing system, antifoam formulation, temperature, and required persistence.
For foam-control applications, viscosity should therefore be considered together with formulation and dispersion behavior, rather than as a standalone specification.
8. Silicone Oil vs. Silicone Antifoam
Neat PDMS Silicone Fluid
This is primarily the silicone fluid itself. It may be suitable for specific applications where direct metering and dispersion are practical.
PDMS-Silica Antifoam
PDMS can be combined with hydrophobic silica to improve foam-control performance. The interaction between the oil and solid particles can contribute to foam-film rupture.
A silicone-based antifoam can also be formulated as an aqueous emulsion, which may simplify dosing and dispersion in water-based systems.
The appropriate form depends on:- Process liquid
- Foam characteristics
- Mixing intensity
- Temperature
- Dosing equipment
- Required active concentration
- Food-use requirements
Therefore, selecting a food defoamer should involve more than simply choosing a silicone oil viscosity.
9. Food Processing Applications
Food and Beverage Processing
- Mixing
- Pumping
- Heating
- Filling
- Fermentation
- Concentration
Controlled antifoam addition can help maintain stable processing conditions.
Oils and Fats
PDMS is recognized as an antifoaming agent for certain food categories involving fats and oils. Codex GSFA provisions specify permitted levels according to individual food categories.
Liquid Food Products
Sauces, syrups, beverages, and other liquid systems can generate foam during high-speed mixing or pumping.
The performance of a silicone defoamer depends on the formulation and on components such as proteins, surfactants, oils, and suspended solids.
Fermentation
Fermentation can produce substantial foam because biological activity and gas generation occur simultaneously.
For food-related fermentation, the selected antifoam must be evaluated against the specific food category, process conditions, and applicable regulatory requirements.
10. How Much Silicone Defoamer Should Be Used?
The required amount depends on:
- Food composition
- Foam severity
- Temperature
- Agitation rate
- Surfactant concentration
- Protein content
- Equipment design
- Antifoam formulation
- Silicone concentration
- Applicable regulatory limits
Codex GSFA gives different maximum levels for PDMS depending on the food category. For example, some current provisions list 10 mg/kg, while other categories have different limits.
The practical target is therefore:
Minimum effective dose + reliable foam control + regulatory compliance
A Practical Process Trial
- Prepare a representative process sample.
- Test several low antifoam concentrations.
- Use consistent agitation or aeration conditions.
- Record initial foam height.
- Measure foam collapse time.
- Observe foam regeneration.
- Check product quality and sensory characteristics.
- Confirm the selected dosage complies with applicable requirements.
This approach provides more reliable results than selecting dosage only from a general supplier recommendation.
11. Food Contact and Regulatory Requirements
Food-use compliance is a critical part of selecting a silicone defoamer.
The FDA lists dimethylpolysiloxane under multiple regulations in 21 CFR Parts 170–186, including 21 CFR 173.340. The FDA also advises users to consult the cited regulation to determine whether the substance is authorized for the intended use.
This means that the term “food grade silicone oil” does not represent unrestricted authorization for every food application.
A practical evaluation should consider:
Product → Composition → Food Category → Function → Dosage → Process Conditions → Applicable Regulation
For international applications, Codex identifies PDMS as INS 900a and provides food-category-specific provisions and maximum levels.
Therefore, buyers should verify the requirements of the actual destination market and application rather than relying only on a general “FDA approved” statement.
12. How to Select Food Grade Silicone Oil for Defoaming
Step 1: Identify the Foam Problem
- During mixing?
- Pumping?
- Heating?
- Fermentation?
- Filling?
Step 2: Analyze the Process Liquid
- Water and oil content
- Protein
- Surfactants
- Salts
- pH
- Solids
- Temperature
Step 3: Select the Product Form
- Neat PDMS
- PDMS-silica compound
- Silicone antifoam emulsion
Step 4: Select Viscosity
- Pumpability
- Metering
- Dispersion
- Spreading
- Persistence
Step 5: Conduct a Process Trial
Compare foam height, collapse time, foam regeneration, and product compatibility under realistic conditions.
Step 6: Verify Documentation
- TDS
- SDS
- CoA
- Product specification
- Recommended dosage
- Food-use or food-contact documentation
- Applicable regulatory references
13. Common Problems with Silicone Defoamers
Overdosing
Increasing the dosage does not necessarily improve foam control. Excessive use can create unnecessary processing and compliance issues.
Poor Dispersion
If the silicone phase is not properly dispersed, it may not reach the foam interface efficiently.
Incorrect Viscosity
A viscosity that is too high may complicate pumping and metering, while a very low viscosity may provide insufficient persistence for some processes.
Wrong Product Form
Neat PDMS, PDMS-silica compounds, and silicone emulsions can behave differently in the same process.
Strongly Stabilized Foam
Protein- or surfactant-rich systems can form highly stable foam films. Strong adsorption layers may reduce the ability of PDMS-based antifoams to spread and enter the foam film.
Regulatory Mismatch
A product may provide excellent technical foam control but still be unsuitable for a particular food application if the permitted use, dosage, or documentation does not match the process.
Conclusion
Food grade silicone oil works as a defoamer mainly through physical and interfacial mechanisms.
The basic process is:
PDMS reaches the foam interface → spreads or enters the foam film → destabilizes the film → promotes film rupture → bubbles collapse.
In PDMS-silica antifoams, hydrophobic silica can further contribute to foam-film destabilization through bridging-related mechanisms.
Defoaming performance depends on more than silicone chemistry. Viscosity, formulation, dispersion, surfactant concentration, temperature, food composition, dosage, and regulatory requirements all influence the final result.
For manufacturers and distributors evaluating PDMS for food-processing foam control, Silico® Food Grade Silicone Oil provides controlled-viscosity PDMS options for selected food-processing and defoaming applications. The appropriate grade and product form should be selected according to the actual process, required foam-control performance, and applicable food regulations.
The key principle is:
Do not select a food grade silicone defoamer by viscosity alone. Evaluate the foam system, product form, application method, dosage, performance, and regulatory requirements together.
Frequently Asked Questions
Food grade silicone oil, typically based on PDMS, reaches the air-liquid interface, spreads or enters the foam film, destabilizes the film, and promotes bubble collapse. PDMS-silica formulations can provide additional foam-film disruption through bridging-related mechanisms.
PDMS has low surface tension, hydrophobicity, and useful interfacial properties. Its surface tension is approximately 21 mN/m at ambient temperature, helping it spread at suitable interfaces.
PDMS can be used as an antifoaming agent in specified food applications. Codex identifies it as INS 900a, while FDA lists dimethylpolysiloxane under several applicable regulations. The exact product, food category, dosage, and use conditions must still be verified.
Not necessarily. Viscosity affects flow, dispersion, spreading, and persistence. The optimum grade depends on the process and antifoam formulation.
Silicone oil generally refers to the PDMS fluid itself. A silicone antifoam may contain PDMS with hydrophobic silica or may be formulated as an emulsion. These formulations can have significantly different foam-control performance.
No. Food-use authorization is application-specific. FDA and Codex provisions identify particular uses and food categories rather than unrestricted authorization for every food application.
Request the TDS, SDS, CoA, product specification, recommended dosage, and relevant food-use or regulatory documentation. The documents should correspond to the intended application and target market.
Silicone Fluid related products
If you want to know other questions about Sillcone Fluid, please contact us and we will provide professional answers.
Popular Recommendations
Get a Catalog & Best Price
- Quick and helpful reply within 24 hours;
- Tailored solutions provided for your project;
- One-stop purchasing service.
Need More Technical Information?
Silico® ORGANOSILICON
- Address: Daiyue Industrial Area, Taian, Shandong, China
- © Copyright 2022 Silico® . All Rights Reserved